15 , October
Silicon-containing aluminum materials are easier to cut than steel but by no means easy to machine as tooling materials. The silicon in these materials acts as a hard abrasive while the aluminum forms a sticky matrix to the cutting edge which can quickly form a built-up edge. Prior to that however, there is very quick degradation in surface finish and dimension.
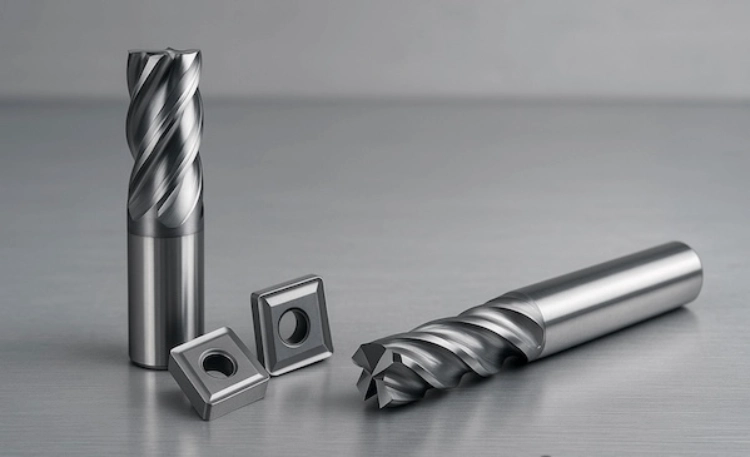
Aluminum solution with diamond coated inserts CVD starts with the alloy, the machining task and the surface finish required. While the CVD diamond coating is able to withstand abrasive stress and to reduce friction, the ideal cutting insert, its preparation and the machine settings are the key to a successful production. TSHZ supplies CVD diamond coated cutting tools and custom profiles for non-ferrous alloys and other abrasive materials.
Why Silicon-Rich Aluminum Needs a Different Insert
Alloys with high silicon content can cause the silicon to cut into the tool edge with every pass. The aluminum matrix can also weld to a hot edge. The result is a combination of wear on the flank of the tool, crater like wear, built-up edge and a dull surface finish.
At first glance the soft workpiece does not give rise to any problems. Tool wear can start off slowly but soon pick up speed once the cutting edge has started to round off. Monitoring finish, burrs and dimensions of parts produced, rather than just the quantity produced, is crucial in establishing a stable process.
What CVD Diamond Does in Aluminum Cutting
TSHZ product information specifies CVD diamond with 9,000-10,000 HV hardness, a friction coefficient of 0.05-0.1 and a thermal conductivity of approximately 2,000 W/(m·K). This information is relevant to the high-silicon aluminum phases since the hard surface contacts the silicon phases and low friction prevents excessive rubbing and built-up edge.
TSHZ materials are deposited as a coating on the tool substrate by means of CVD process. The coating thickness can be easily controlled within a range of 1 μm to 30 μm on complex cutting tool edges. The insert geometry must remain sufficient to grant appropriate clearances, adequate chip control and sufficient edge sharpness after coating.
Choose the Insert by Operation
Turning and facing
For turning, consider starting with the surface already machined, and cut in the direction of the principal cutting force. A sharp positive cutting edge helps to reduce cutting force and prevents aluminum from sticking to the insert. Also be sure that the insert is securely clamped in the holder – vibration will show up as repeated scratches on the surface.
The CVD diamond coated cutting inserts page shows the direct TSHZ product for non-ferrous metal machining. Check insert shape, nose radius, substrate and coating specification on the drawing against the shown product.
Milling pockets and faces
By milling, you are generating interrupted cuts that vary in chip thickness. Keep your tooling as short as possible and make sure your workholding is solid. Check to see if chips will clear your pocket cavity without re-cutting them. If not, a harder insert will only increase heat and rubbing caused by poor evacuation of the previously generated chips.
A custom profile is useful for a special shoulder, form or small radius. TSHZ’s custom CVD diamond tool service supports non-standard geometries when an off-the-shelf insert does not hold the required profile.
High-finish components
High gloss aluminum surfaces have very sensitive edges and require a consistent nose radius. Finish light and keep the settings the same for the finishing pass. Do not run mixes of tools with different edge preparation in production and measure the first part off and the part that is produced near the tool’s planned replacement.
Geometry and Edge Preparation Checks
Do not select an insert from the material name alone. List out Alloy grade, Silicon % and Stock allowance and Toolholder & Spindle rpm & Feed per tooth or Feed per revolution & Radial depth of cut & Coolant/Air etc. These parameters define whether the edge is cutting or rubbing.
A larger nose radius will help to provide a smoother surface but may increase cutting force. Very sharp edges cut well but are not so good when there is any vibration or the cutting is intermittent. The nose radius and edge finish must be chosen to match the work being machined and the machine that is being used to do the work.
CVD coating should be uniform. Thickness of the coating as well as edge radius of coating should be inspected. For repeated orders, same reference for inspection should be used for the first as well as for the last batch to ensure same behavior of the first and last part of the order.
Controlling Built-Up Edge and Heat
Built-up edge is often a sign of friction, heat or a cutting edge that is no longer sharp. Start by checking chip flow and cleaning the holder. Use air or suitable coolant according to the machine and alloy process. Keep the cutting edge engaged consistently; rubbing at the bottom of a pocket can create more heat than a heavier but stable cut.
Cloudy surface? Check edge under magnification before changing all cutting parameters. A small deposit can often be removed by improving the chip removal. A rounded edge or coating damage requires a new insert.
Cost per Part Is the Useful Measure
Diamond-coated inserts cost more than standard carbide inserts. The comparison should include insert price, usable parts per edge, changeover time, surface rework, scrap and machine availability.
A controlled trial is best. Run the same alloy, same toolpaths, same inspection methods and measure things like percentage of good parts, average surface finish, dimension shift and time spent in swapping out or modifying inserts. Then purchasing and production have a basis for their decision that the other can understand.
A Simple Trial Plan for a New Insert
Start testing with a meaningful part section, not with a small test coupon that doesn’t reproduce the realistic process conditions for heat and chip load. Note the alloy temper, silicon content, stock allowance, etc. as well as the toolholder used for testing. Make sure the toolholder is clean and the spindle is checked for runout before the first cut to rule out any potential setup problems that could be misinterpreted as insert wear.
The first part should be inspected for surface quality, burrs and dimensions. The same checks should be repeated after a certain number of parts have been produced. Subsequently, the check should be repeated when the surface starts to change. The cutting data must remain unchanged for the comparison. Only with supplier’s documented change to the cutting data the results can also be used by production and purchasing.
Photo the edge before cleaning any stick-on if there is any. A soft aluminum-like deposit with a rounded edge and coating damage is likely to have one of several causes. Thus matching the correction to the cause is more likely to save time than reduce speed and change inserts prematurely.
When Custom TSHZ Inserts Make Sense
Request a custom insert when the part needs an unusual nose radius, a special form, a small feature or a coating thickness matched to a tight tolerance. Provide the alloy chemistry, drawing, machine, holder, cutting data and current failure mode.
TSHZ’s diamond coated insert product page and custom profile service provide the right starting points for a technical review. For a sample or application recommendation, send the drawing through the TSHZ contact page.
FAQ
Are CVD diamond inserts suitable for all aluminum alloys?
They are intended for abrasive non-ferrous materials, but alloy chemistry, silicon content, interrupted cutting and machine rigidity still matter. Confirm the insert grade and edge preparation on the actual alloy.
How can I reduce built-up edge in high-silicon aluminum?
Keep the edge sharp, control heat, improve chip evacuation and avoid rubbing at low engagement. Inspect the insert before making large changes to speed or feed.
How often should diamond coated inserts be replaced?
Use surface finish, burrs and dimensional drift as the replacement criteria. A fixed part count is only a starting point because alloy, engagement and machine condition change tool life.